Pipe support systems rarely fail in one dramatic moment. A loose clamp, corroded shoe, or blocked guide can begin quietly. Later, the pipe may vibrate, sag, or transfer unexpected loads to connected equipment. That is why learning how to maintain pipe support systems matters in every process plant, refinery, power station, and commercial facility.
The U.S. Department of Energy’s Operations and Maintenance Best Practices Guide identifies preventive maintenance as a major source of reliability and operating-cost improvement. NACE International’s IMPACT study also estimated global corrosion costs at about $2.5 trillion annually, equal to roughly 3.4% of global gross domestic product. These figures do not measure pipe supports alone. They show the wider cost of neglecting steel, coatings, drainage, and inspection access. API RP 574 and ASME B31.3 provide useful inspection and piping-integrity frameworks, but neither replaces competent field judgment.
George A. Antaki, a recognized piping engineer and author, offers a practical warning: “The best piping design is one that remains reliable throughout its operating life.” That principle should guide every support inspection. Look beneath insulation. Check for rust around anchor plates. Watch for shiny wear marks, cracked welds, missing bolts, and water trapped near shoes. Small findings matter.
No checklist is perfect. A support can look sound and still carry an altered load. Temperature changes, vibration, chemical exposure, and nearby construction may change its behavior. The following ten practices combine documented standards, maintenance experience, and careful observation. They are not a substitute for an engineered assessment, but they create a stronger starting point.
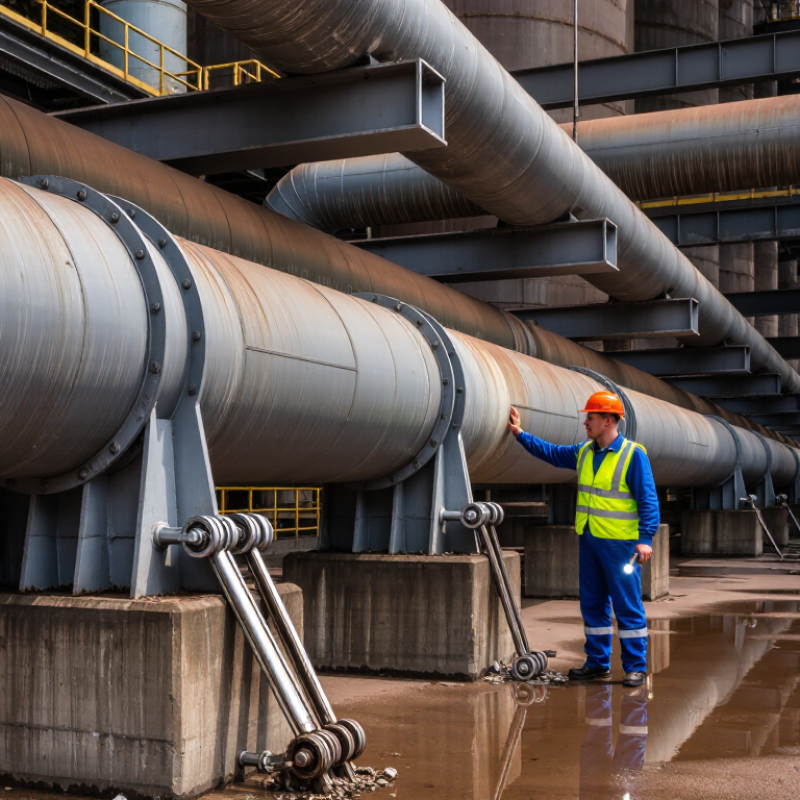
Top 10 Ways to Maintain Pipe Support Systems
Reliable pipe support begins with correct load classification under ASME B31.1. Treat pipe weight, insulation, fluid, valves, and connected equipment as sustained loads. Thermal expansion creates displacement and stress. Occasional loads may include wind, seismic effects, relief reactions, or water hammer. Dynamic loads need special attention. They can damage supports quickly. MSS SP-58 helps engineers select suitable support types and materials, but it does not provide one universal spacing rule. Spacing depends on pipe diameter, wall thickness, temperature, material, insulation, and concentrated loads.
In practice, calculate support spacing between anchors, guides, and sliding points. Place supports near heavy valves and changes in direction. Allow thermal movement without forcing the pipe into equipment nozzles. Check spring supports where vertical movement is significant. Inspect shoes, clamps, welds, and base plates for corrosion, distortion, and loose hardware. A line may look straight while carrying excessive stress. I have seen field changes create unsupported spans that were absent from the original drawing. That mistake deserves review, not blame.
Tips: Mark each support with its function and design load. Recheck spacing after insulation, hydrotesting, or valve replacement. Keep inspection records with temperature and operating conditions. Do not copy spacing from a nearby line. Similar pipes can behave differently. Experienced reviewers should confirm calculations, field measurements, and actual movement before approving modifications.
| No. | Maintenance Practice | Pipe Load Classification | Support Spacing Guidance | Inspection and Engineering Checks | Acceptance Indicators |
|---|---|---|---|---|---|
| 1 | Establish a support register Assign an identification number and location to every hanger, shoe, guide, anchor, and spring support. |
Deadweight loads, operating loads, occasional loads, and displacement-related loads. | Record the actual spacing between supports and compare it with the approved stress-analysis model and layout drawings. | Verify pipe size, material, insulation thickness, fluid density, operating temperature, and support type. | Each support is traceable, correctly located, and consistent with the design documentation. |
| 2 | Control deadweight loading Inspect the combined weight of pipe, fittings, valves, insulation, and contained fluid. |
Primary sustained load: pipe self-weight plus contents and permanently attached components. | Typical preliminary spans for horizontal steel pipe may range from approximately 1.8 m for small-bore pipe to 5.5 m for large-bore pipe; use project span calculations for final values. | Check bending stress, shear, local wall stress, vertical deflection, support reaction, and concentrated valve loads. | No excessive sagging, support overload, cracked welds, or local pipe deformation is present. |
| 3 | Inspect thermal movement provisions Confirm that sliding shoes, guides, loops, and anchors permit the intended expansion. |
Thermal displacement loads, friction loads, anchor loads, and guide reactions. | Reduce spacing or add guides near changes in direction, expansion loops, anchors, and equipment connections when required by the analysis. | Check cold-to-hot movement, guide clearances, sliding surfaces, anchor integrity, and friction assumptions. | Movement is unrestricted where intended; guides do not bind and anchors do not show distress. |
| 4 | Verify spring supports Inspect variable- and constant-effort spring hangers for correct setting and travel. |
Sustained weight combined with thermal vertical movement. | Spring locations and spacing must follow the pipe stress-analysis results, especially near heavy valves and vertical offsets. | Check hot and cold positions, load settings, travel stops, corrosion, alignment, and hanger rod condition. | Operating position is within the specified range and temporary travel locks are removed after commissioning. |
| 5 | Provide special support for concentrated loads Review valves, strainers, flanges, instruments, vents, drains, and inline equipment. |
Localized deadweight, operating reaction, vibration, and maintenance handling loads. | Use a support close to heavy components when practical; do not rely only on long-span pipe flexibility to carry concentrated loads. | Check flange alignment, nozzle loads, support accessibility, removable components, and maintenance clearance. | Equipment nozzles remain aligned and components can be removed without overstressing the piping. |
| 6 | Separate support functions Maintain the distinction between rests, hangers, guides, line stops, and anchors. |
Vertical, lateral, longitudinal, thermal, seismic, and dynamic loads. | Place guides and stops according to calculated movement and reaction forces rather than using uniform spacing alone. | Confirm that each support performs only its intended restraint function and that clearances are maintained. | No unintended restraint, pipe lift-off, binding, or overstressed structural attachment is observed. |
| 7 | Inspect vibration and dynamic effects Check lines connected to pumps, compressors, turbines, safety valves, and two-phase services. |
Fluid-induced vibration, pressure thrust, relief-valve reaction, water hammer, and slug-flow loads. | Use shorter spans and additional restraints where vibration or transient analysis identifies elevated dynamic response. | Look for fretting, loose clamps, fatigue cracks, abnormal noise, impact marks, and repeated bolt loosening. | No visible vibration damage; dynamic supports and restraints remain tight and correctly aligned. |
| 8 | Protect insulation and corrosion barriers Inspect pipe shoes, wear pads, saddles, clamps, and insulation weatherproofing. |
Deadweight loads combined with local contact pressure and environmental degradation effects. | Support spacing must prevent insulation crushing and keep contact pressure within the approved support-detail limits. | Check moisture ingress, corrosion under insulation, damaged wear plates, sharp edges, and missing protective coatings. | Insulation remains continuous and dry; support contact areas show no unacceptable corrosion or crushing. |
| 9 | Review structural attachments Inspect welded attachments, clamps, threaded rods, beam connections, and concrete anchors. |
Support reaction forces, thermal restraint forces, seismic loads, wind loads, and occasional loads. | Support spacing must be coordinated with the capacity of the supporting steel, concrete, and connection details. | Check weld condition, bolt torque where specified, anchor edge distance, corrosion, deformation, and load path continuity. | Connections are secure, undamaged, adequately supported, and consistent with the approved design. |
| 10 | Revalidate after modification or abnormal service Repeat the support review after rerouting, insulation changes, trips, water hammer, or seismic events. |
Combined sustained, thermal, occasional, dynamic, and abnormal-event loads. | Recalculate spacing and reactions whenever pipe weight, temperature, routing, fluid service, or support configuration changes. | Compare field conditions with updated isometrics, flexibility analysis, support schedules, and inspection findings. | Updated records are approved, deficiencies are corrected, and the piping system remains within design limits. |
Moisture can remain trapped beneath saddles, clamps, and shoes. Hidden corrosion may deepen while nearby steel looks dry. A clean surface proves little. Inspect crevices and low points during scheduled maintenance.
Check support contact points, welds, clamps, saddles, and drainage paths. Look for wet debris, cracked coatings, rust staining, and shiny wear marks. Some hidden areas are easy to overlook.
Use suitable coatings, effective drainage, and planned inspections. Repair damaged coating after proper surface preparation. Electrical isolation can reduce corrosion between different metals. Verify the repair procedure before work begins.
Use calibrated ultrasonic equipment at support contact points. Record each location, reading, date, and calculated corrosion rate. Compare readings with the engineering minimum wall thickness. Visual judgment is not enough.
Qualified engineers should assess remaining life and repair requirements. Do not rely on one reassuring reading. Repeat measurements when uncertainty exists. Weak evidence should remain visible in the maintenance plan.
Reassess them when estimated loading exceeds 10 percent of the design load. Added valves, thicker insulation, or changed fluid density can increase loading. Review spacing, anchors, guides, shoes, welds, and nearby structures.
Watch pumps, elbows, reducers, and unsupported branch connections for shaking. Loose clamps may produce metallic tapping sounds. Look for sagging, displaced restraints, cracked coatings, and polished wear marks. Vibration can expose problems that static calculations miss.
Do not remove a support casually. Load transfer may create a greater hazard elsewhere. Over-tightening can restrict thermal movement and stress the pipe. Check expansion, operating conditions, and load paths first.
Include operating temperature, pressure, fluid contents, insulation, and temporary maintenance equipment. Compare drawings with actual field conditions. Document every change, even small ones. Human judgment can miss gradual load growth.
Recheck the system after startup, shutdown, and significant process modifications. Confirm that guides, anchors, and flexible connections work as intended. A second review is wise. My earlier inspection focused on corrosion and missed vibration, so the repair took longer.
Maintaining pipe support systems requires a structured approach that begins with classifying operating, thermal, and occasional loads, then setting support spacing according to applicable engineering requirements. Regular inspections should verify pipe alignment, settlement, support condition, and required clearances at scheduled intervals, with reviews conducted as often as five years or sooner when service conditions demand. Corrosion control is also essential: exposed supports and piping should be monitored, protective measures applied, and wall thickness confirmed to remain within safe design limits.
To understand how to maintain pipe support systems effectively, operators should manage thermal expansion through properly positioned guides, anchors, and sliding supports while keeping flexibility within approved limits. Vibration, rubbing, looseness, and abnormal movement should be addressed promptly. Whenever modifications or process changes increase design loads by more than 10 percent, the support arrangement should be reassessed. Accurate records, qualified inspections, and timely corrective actions help preserve system reliability, reduce unexpected failures, and extend service life.
 Ampy Pipe